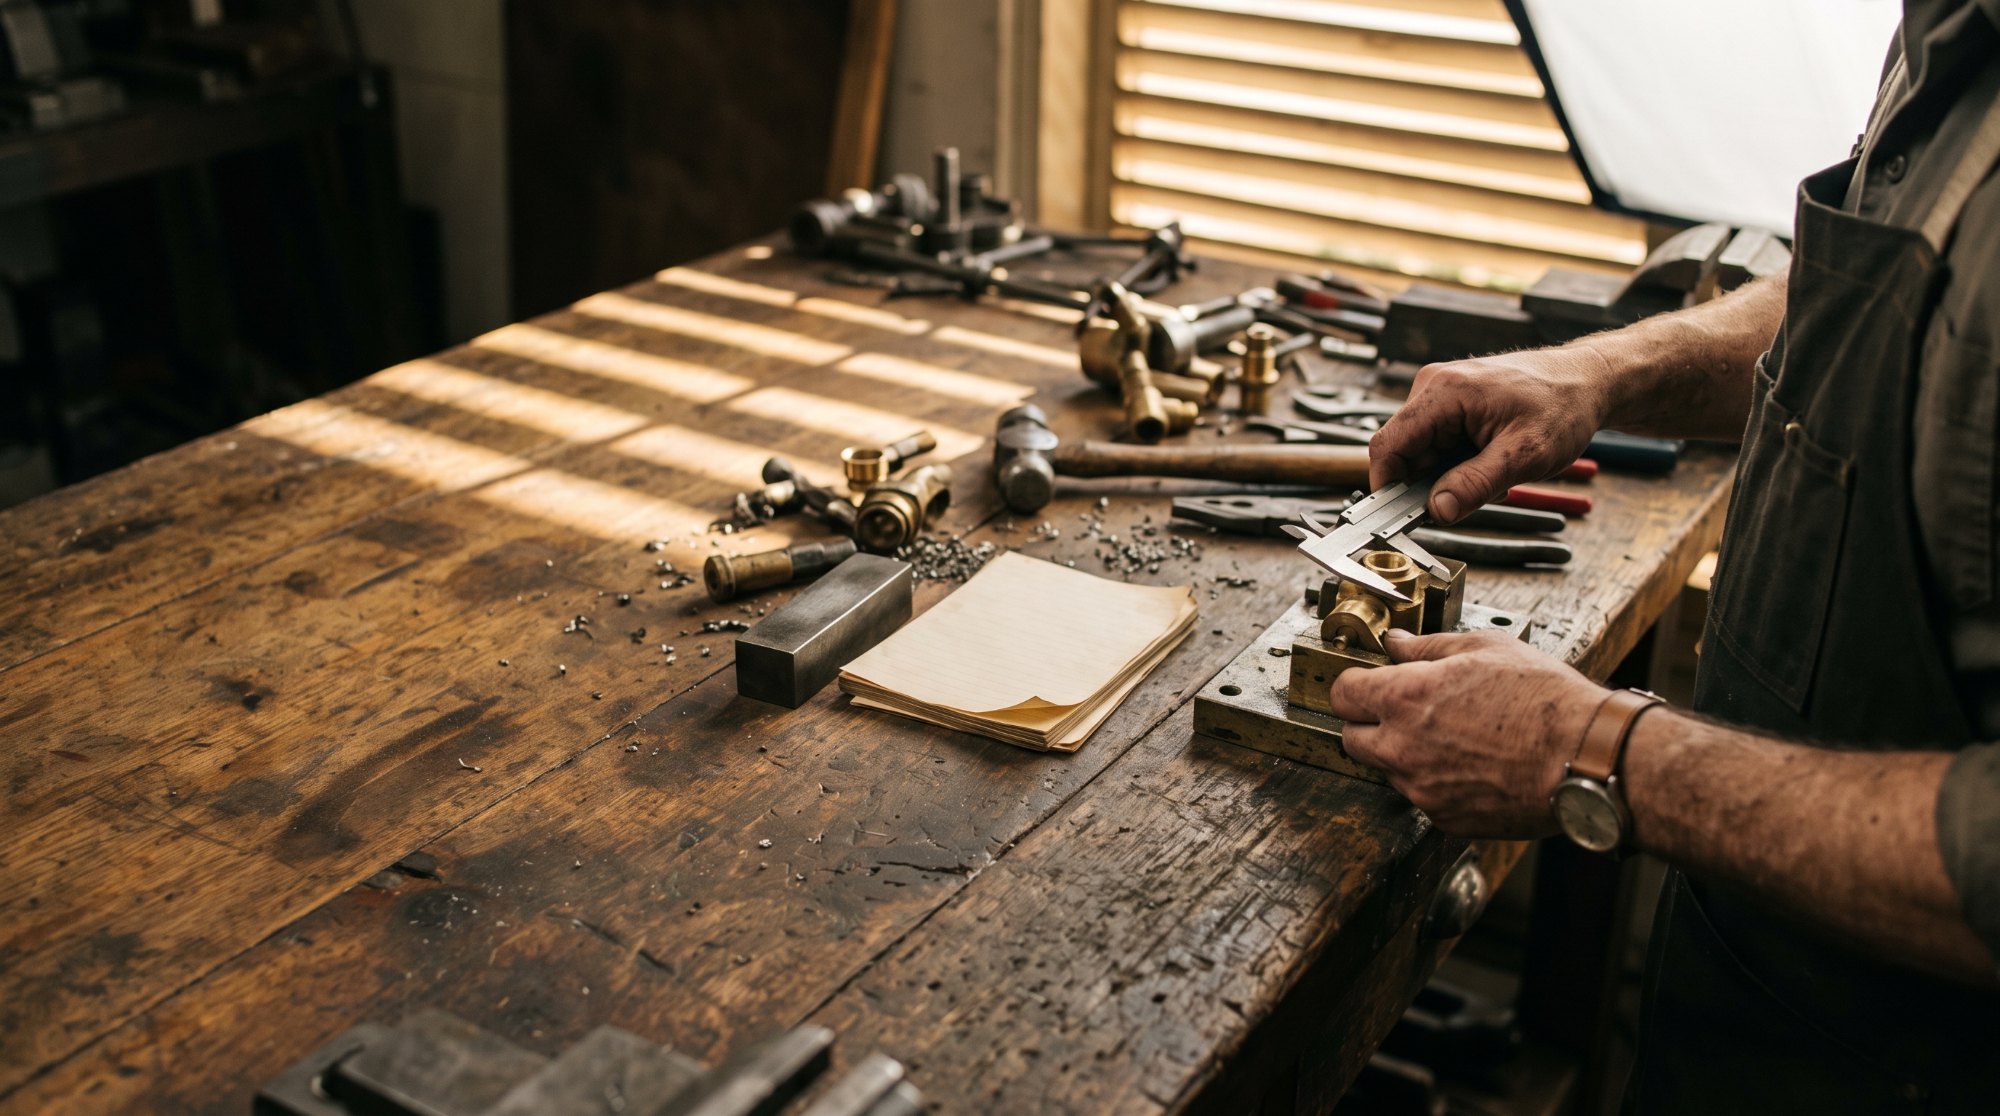
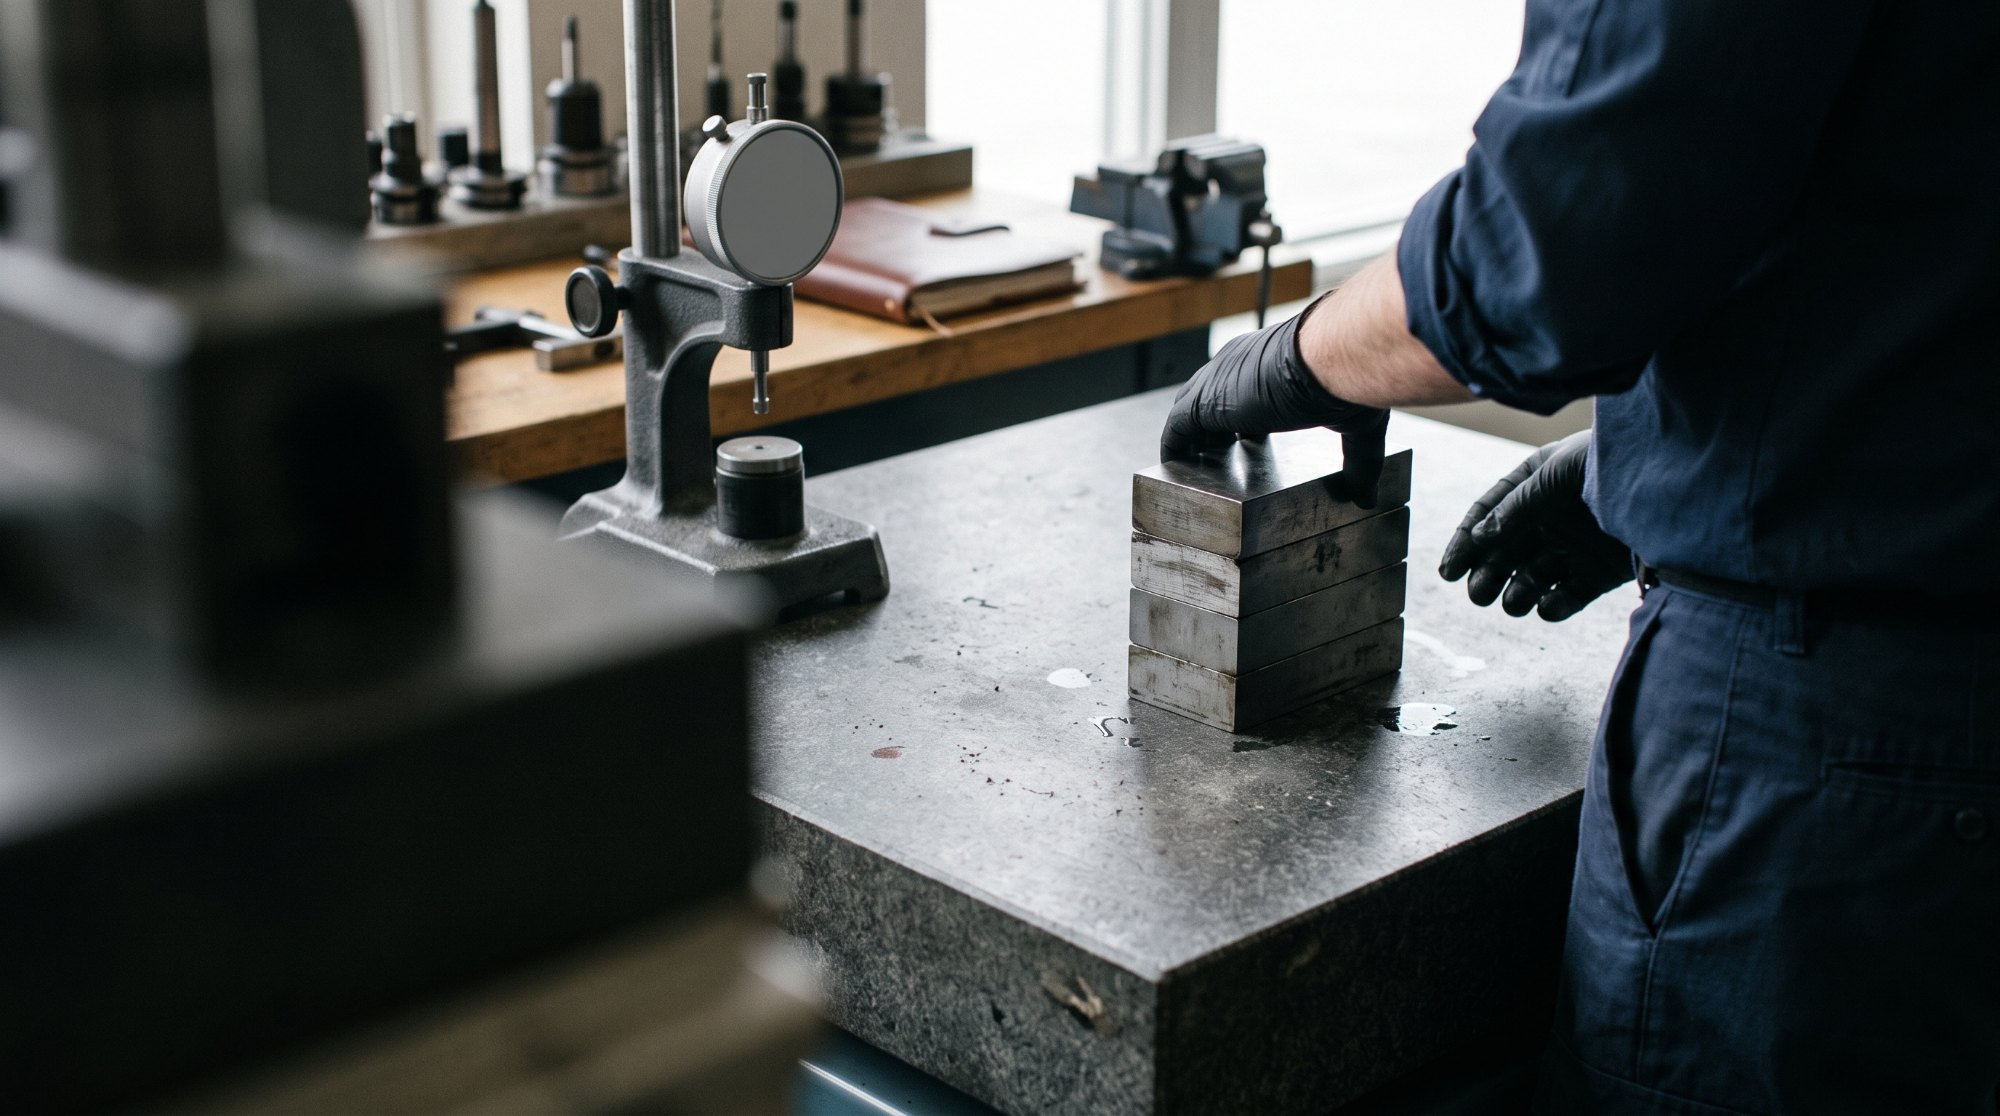
On any calibration bench in Coimbatore, the same small drama repeats a dozen times a day: an inspector picks up two gauge blocks, wipes them, touches them together with a twist — and the second block hangs off the first with no support at all. No clamp, no adhesive, nothing between them but a film far thinner than a wavelength of light. The question people ask about this — why do gauge blocks stick together when stacked? — sounds like curiosity. In practice it is the front door to one of the most useful skills in dimensional metrology, because a stack that is not wrung properly is not a stack. It is two pieces of steel leaning on each other, and every measurement built on it inherits the gap.
This guide explains what the wringing film actually is, why cleanliness decides whether it forms at all, how to wring and separate blocks without damaging them, and what a failed wring is telling you about the faces. It complements our gauge block stack error guide, which covers how much error each step in a stack adds once the blocks are properly joined.
Gauge block faces are lapped to sub-micron flatness and finished to a mirror. When two such faces meet with only a microscopic film of fluid between them, three effects combine: molecular attraction between surfaces close enough to interact, the surface tension of the film, and atmospheric pressure acting on the joint once the air is excluded. None of these is glue. Together they produce a joint that holds the blocks firmly, resists shear when you try to slide them, and lets light pass through the faces with almost no distortion — which is why an optical flat can still read through a properly wrung stack.
The film itself is not something you apply. It is whatever remains on the face after cleaning: a residue of the solvent, the natural oxide layer, a few molecules of everything the surface has touched. The art of wringing is partly the art of controlling that residue. Too much fluid and the blocks slide without gripping; too little and the faces are dry enough to score each other. The classic feel to aim for is light resistance, like sliding through butter — smooth, with a clear increase in drag as the faces come into full contact.
A wring that will not take usually has nothing to do with technique. It has to do with what is on the faces. A fingerprint carries enough skin oil to keep two faces apart by more than the film can bridge. A dust particle the eye can barely see will hold the blocks apart at that point and raise a false reading through the whole stack. Rust bloom, even invisible, ruins both the wring and the face.
The routine that works on a real bench:
Storage discipline feeds this directly. Blocks kept in foam-lined cases with desiccant arrive at the bench ready to wring; blocks kept loose in a drawer arrive already defeated. Our gauge storage guide covers the case, the environment, and the labelling habits that make the difference.
The motion has a sequence, and the sequence matters:
Never force a wring. Pressure that exceeds a light twist-and-slide does not improve the joint; it risks scoring both faces if anything hard is trapped between them, and scored faces never wring properly again without lapping.
The joint is designed to resist tension along the axis — so do not pull straight apart. Slide the blocks sideways, or use the sliding-and-twisting motion in reverse. The blocks part with a small click and no drama. Pulling stacks apart axially can chip edges, and an edge chip is where corrosion starts and where stacks begin seating badly.
Equally important: do not leave blocks wrung together. A joint left overnight in humid air can seize by corrosion, and separating it tears the faces. At the end of the work, take the stack down, wipe the faces, oil lightly if the storage area is not climate-controlled, and return the blocks to the case. This habit alone prevents most of the permanent damage we see in gauge sets brought in for recalibration.
Dimensional standards reference 20 °C, and a gauge block taken from a case in a 32 °C shop is not at 20 °C — it is a few tenths of a percent of a percent away in a direction you will not see. Let blocks and the workpiece equalise on the bench or a granite surface plate before measuring; the soak time depends on the mass, but minutes, not seconds. Our article on the micron error at 32 °C covers what this does to readings when it is ignored, and the IS 3455 reference-temperature cases in our IS 919 / IS 3455 guide put the rule in standards terms.
Every wring and every separation cycles the faces. In a set used daily, the blocks you reach for most wear first. That is what wear blocks are for: a pair of sacrificial blocks placed at the ends of the stack, taking the handling and the contact so the calibrated blocks in the middle do not. When a wear block's faces degrade, you replace one inexpensive block instead of re-lapping or retiring the set.
If you are specifying a set, check that wear blocks are included and that their size matches the stack lengths you actually build. Our guide to setting masters covers the reference side of the same discipline.
Blocks that refuse to wring after proper cleaning are not being difficult. They are reporting:
Any of these is a reason to send the set for calibration rather than to press harder at the bench. A set that wrings inconsistently can still pass a casual size check and still poison a stack. Our repeatability study guide is the quick test that catches this.
We supply precision gauges and reference hardware for dimensional measurement, and we support calibration planning so that gauge blocks, setting masters, and working gauges stay on a documented recall programme rather than an ad-hoc one. If your gauge blocks wring inconsistently, or your stack results stopped agreeing with your references, talk to our team — the cause is usually visible in the first five minutes on the bench.
Most gauge mistakes are not exotic — they are the same handful of habits repeated across every shop. A field guide to the errors that quietly corrupt inspection, and the fixes that cost nothing.

Automotive runs on volume and consistency — thousands of parts, every one the same. How precision gauging holds the supply chain together and what automotive inspection demands of a gauge.
A shop-floor guide to building a wrung gauge block stack you can trust: grade selection per ISO 3650, wringing film thickness variability, thermal soak times by material, stack-building rules, and